
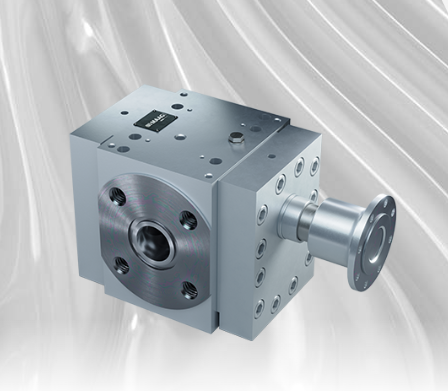
Why Recycling and Regrind Lines Struggle
Recycling lines operate with more variability than virgin material extrusion. Contamination, variable flake or pellet quality, fillers, degraded polymer, and changing viscosity all make stable extrusion harder to maintain. Without the right melt-delivery system, pressure swings, frequent screen changes, and downtime become common.
Contamination Load
Paper, aluminum, gels, black specks, fines, and degraded material shorten screen life and affect product quality.
Pressure Instability
Variable feed and contamination loading create unstable pressure, pulsation, and harder-to-control extrusion conditions.
Frequent Interventions
Manual screen changes, downtime, and cleaning events can limit throughput and increase operator burden.
Material Variability
Regrind, reclaimed streams, and post-consumer material require more forgiving process equipment and better filtration strategy.
How Recycling Melt Delivery Systems Work Together
In recycling applications, the strongest results come from treating the line as a connected system instead of relying on one device to solve everything. Melt pumps stabilize pressure and flow. Screen changers and self-cleaning filters remove contamination before it reaches the die. Controls help maintain repeatable conditions. Flow distribution components support more complex layouts. Support carts, drives, and integrated assemblies simplify retrofit and installation.
Upstream
Conveying, blending, feeding, and material preparation affect the consistency of the recycled stream entering the extruder.
Melt Delivery
Pumps, screen changers, filters, controls, and adapters determine pressure behavior, contamination removal, and process stability at the die.
Downstream
Measurement and inspection systems verify what the line is actually producing and help confirm quality improvement after process changes.
Choosing the Right Melt Pump & Filtration Strategy by Application
Melt pumps, screen changers, and filtration systems are not one-size-fits-all. The right configuration depends heavily on the application, material consistency, contamination level, and process stability requirements. The table below highlights how these systems are typically applied across recycling, film and sheet, and pipe and profile extrusion lines.
| Application | Primary Goal | Melt Pump Role | Filtration Strategy |
| Recycling & Regrind | Contamination removal and uptime | Stabilize pressure with variable material streams | Self-cleaning melt filters for heavy contamination loads |
| Film & Sheet | Gauge uniformity and thickness control | Meter melt flow and reduce thickness variation associated with mass-flow or die-pressure changes. Cross-web profile requires separate review of the die, cooling and related process conditions. | Continuous screen changers or fine filtration for clean melt |
| Pipe, Tubing & Profile | Dimensional stability: outside diameter (OD), inside diameter (ID), and wall thickness | Reduce pulsation and maintain steady flow into the die | Screen changers or filtration depending on cleanliness |
Melt Pumps for Recycling and Regrind Extrusion
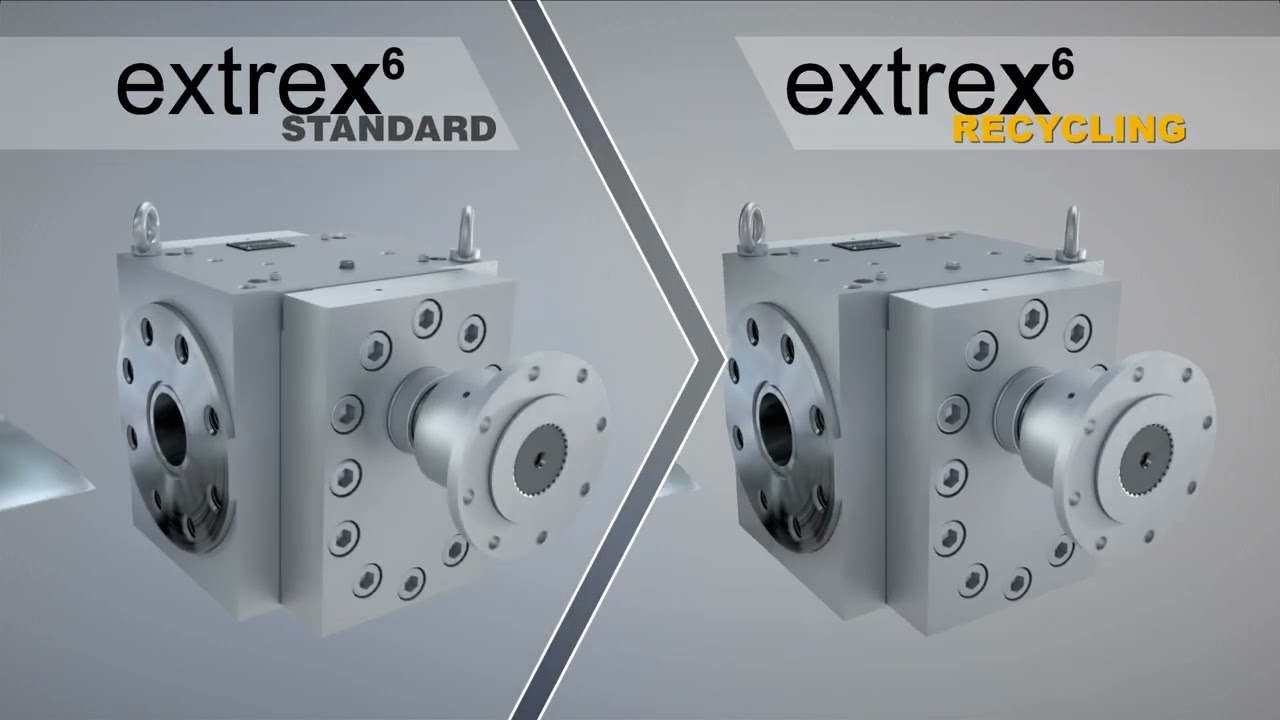
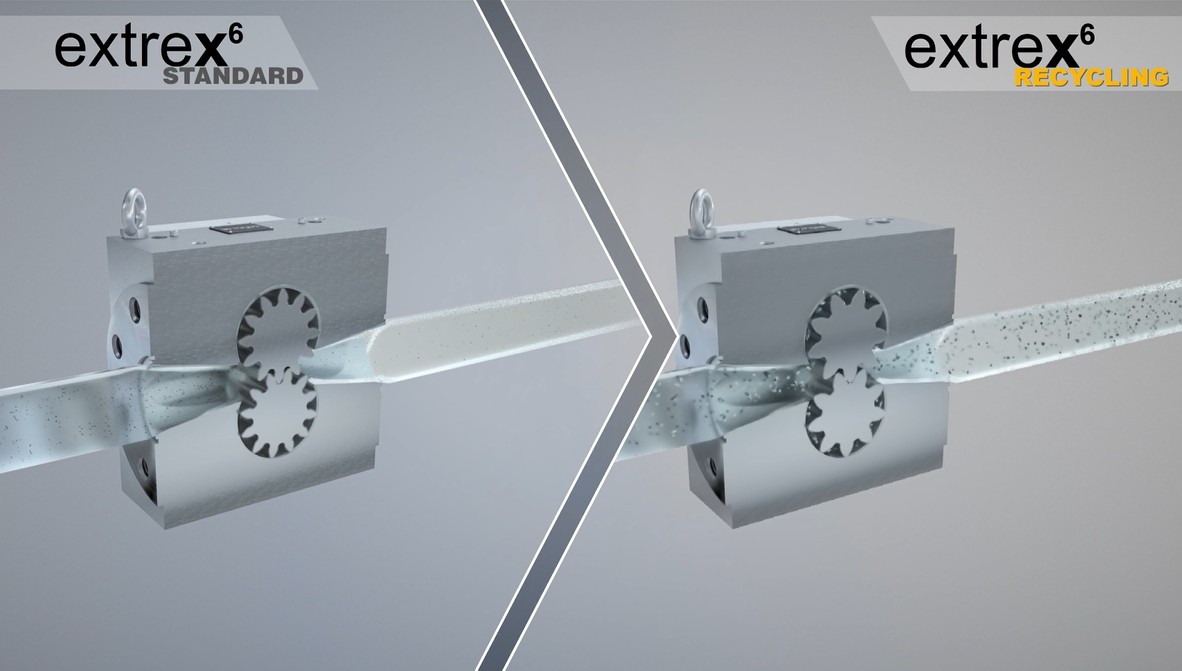
In recycling extrusion, melt pumps are used to stabilize pressure, reduce pulsation, and improve process consistency when material quality changes from lot to lot. By shifting pressure generation away from the extruder and into a precision gear pump, the system can run with more repeatable flow and better control at the die.
This matters because recycled and reclaimed streams often create more variability than virgin material. A properly selected pump can help improve process stability, reduce pressure swings, support higher throughput, and make the rest of the line easier to control.
- Stabilize pressure and flow with variable material quality
- Reduce pulsation and improve downstream consistency
- Support higher throughput with better process control
- Improve reliability on regrind, reclaimed, and filled materials
Screen Changers for Controlled Recycling Streams
Screen changers still have a place in recycling, especially on cleaner, controlled, or pre-filtered material streams. They help protect the die and downstream process by removing contamination before it reaches the most sensitive parts of the line.
For heavier contamination loads, self-cleaning filters are often the better answer. But on the right recycling application, continuous or simpler screen changer designs can still support more stable pressure and practical contamination control.
| Continuous Screen Changers | Manual / Simpler Systems |
| Better uptime | Lower complexity |
| Better for controlled contamination loads | Better for simpler lines or lighter duty use |
| Useful where uptime matters more than the simplest initial setup | Useful where operator intervention is acceptable |


Self-Cleaning Melt Filtration for Heavy Recycling Contamination
On real-world recycling lines, standard screens often struggle because contamination loading is too high or too inconsistent. This is where self-cleaning and high-performance melt filtration becomes critical. Dedicated recycling filters can remove contamination continuously while maintaining throughput and reducing operator intervention.
This matters when processing post-consumer plastics, regrind, filled compounds, and streams containing paper, aluminum, fines, gels, or degraded material. Proper melt filtration can extend service intervals, improve uptime, and protect downstream equipment from contamination-related instability.
- Designed for heavier contamination loads than standard screen packs
- Support continuous operation on difficult recycling streams
- Reduce manual cleaning and frequent changeovers
- Improve uptime, product consistency, and downstream protection
Pump Drive and Control Systems
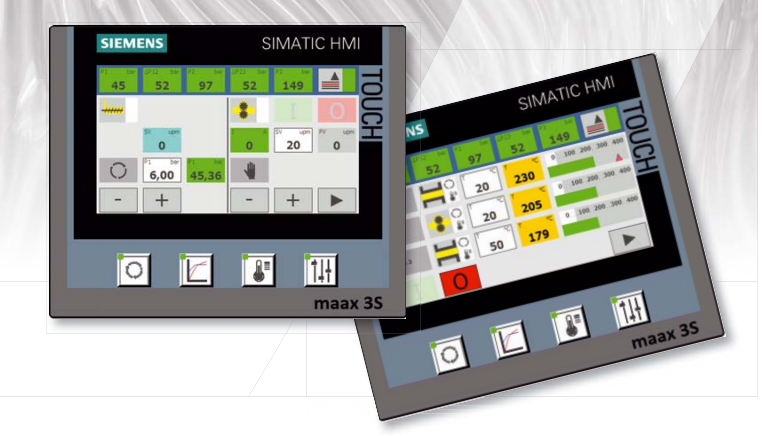
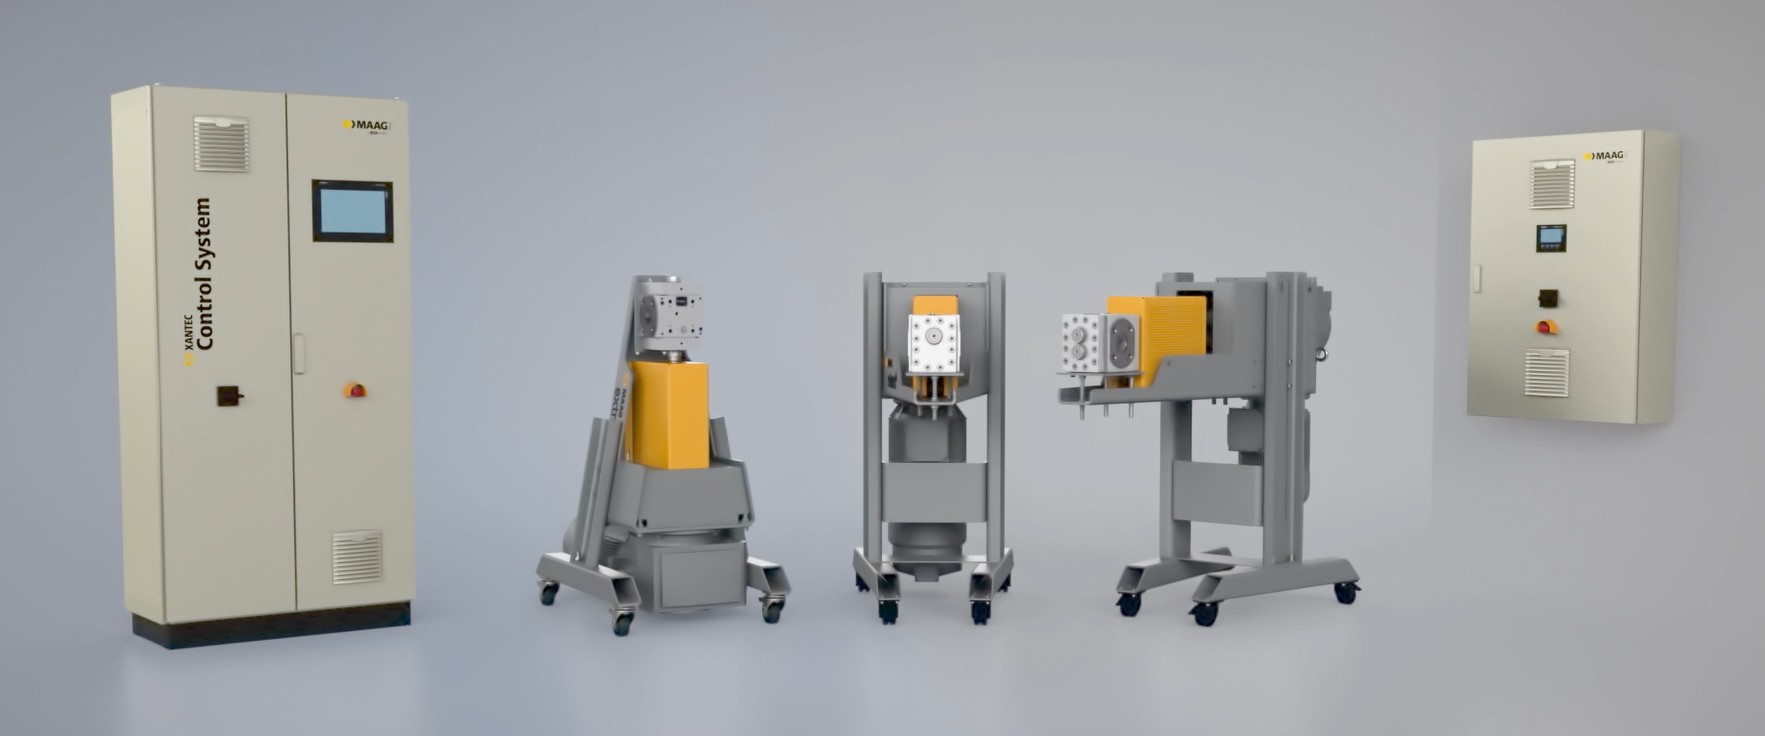
Good hardware still needs good control. Drive and control systems help manage pump speed, pressure behavior, temperature monitoring, startup sequences, and production stability. In recycling, this can be especially important because the process window is often narrower and material variability is higher.
Integrated monitoring also makes troubleshooting faster and provides better visibility into how the line is responding to changing contamination loads and variable feed quality.
Flow Distribution and Flexible Recycling Line Layouts
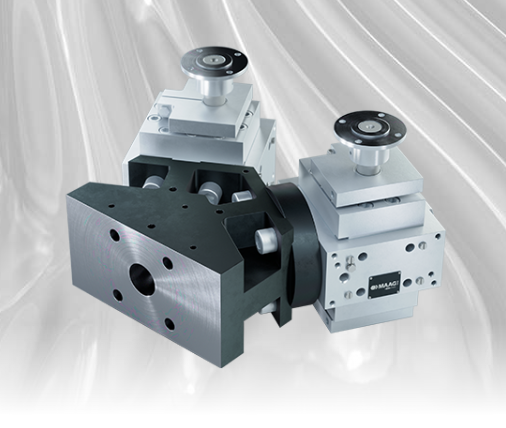
Flow distribution components can help split or direct melt streams on more complex recycling lines. Address contamination first, then review flow distribution as part of the complete melt-delivery system.
For engineers evaluating larger or more integrated recycling lines, a Y-adaptor or related distribution component becomes part of the pressure and flow strategy that influences how material is delivered downstream.
Complete Melt Delivery and Retrofit Systems
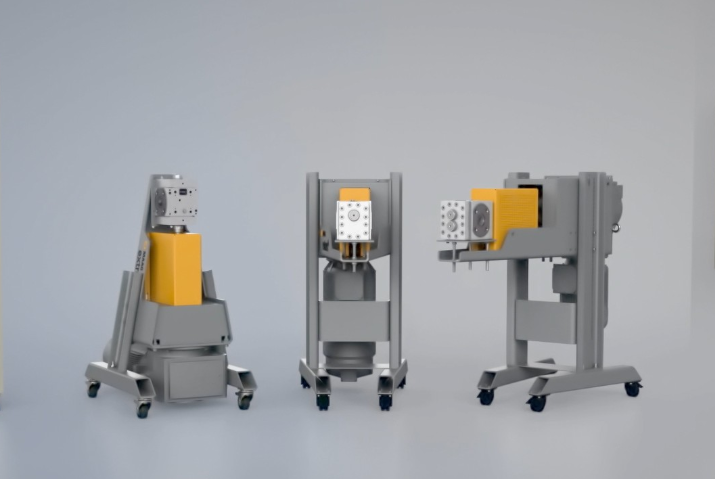
Some recycling projects are not about a single product. They are about how the pump, filtration, controls, drive units, support structures, and line integration work together. Integrated melt delivery systems make sense when the goal is to reduce installation complexity, improve serviceability, and create a more repeatable process package.
This is especially useful in retrofit applications where mechanical fit, control strategy, and maintenance access matter almost as much as the equipment selection itself.
Selected Reading and Videos
How MAAG Pumps Improve Output and Product Consistency
Background on pressure stability, pulsation reduction, and how melt pumps improve extrusion performance.
Watch Extrex Recycling Pump Video
Supplemental video resource focused on melt pump technology for recycling and reclaimed material extrusion.
Watch Recycling Pump and Filtration Overview
Overview animation covering how melt pumps and filtration systems fit together on recycling lines.
Tools for Recycling & Regrind Process Evaluation
Melt Pump Sizing Calculator
Estimate melt pump flow rate, pressure requirements, and pump type based on polymer, throughput, and process conditions.
Filtration & Screen Changer Selector
Identify the right screen changer or melt filtration system based on contamination level, material variability, and process goals.
Polymer Filtration and Melt Pump ROI Calculator
Estimate the financial effect of improved melt delivery, reduced downtime, and higher uptime on recycling lines.
Cpk / Ppk Process Capability Calculator
Useful when evaluating process variation, consistency, and stability across recycled material streams.
Extrusion Throughput and Line Speed Calculator
Connect throughput, output, and line speed assumptions when evaluating recycling and regrind extrusion performance.
Engineering FAQ: Recycling and Regrind Melt Delivery
Can a melt pump correct a cross-web thickness profile?
A melt pump meters flow and can reduce variation associated with pressure or mass-flow changes. A cross-web profile problem requires separate review of die distribution, cooling and other process conditions.
Why use a melt pump on a recycling line?
A melt pump helps stabilize pressure and flow when recycled material quality changes, which can improve process consistency, reduce pulsation, and support more repeatable extrusion.
Do screen changers and self-cleaning filters do the same thing?
Not exactly. Both remove contamination, but self-cleaning melt filters are often better suited for heavier, more variable contamination loads found on many recycling lines.
When can a screen changer still make sense in recycling?
Screen changers can still fit cleaner, controlled, or pre-filtered streams where contamination loading is lighter and the process does not require a fully self-cleaning filtration strategy.
Why is self-cleaning filtration important in recycling?
Because heavier contamination loads can shorten screen life and force frequent interventions. Self-cleaning filtration helps maintain throughput, reduce downtime, and extend service intervals.
What problems does melt filtration solve on recycling lines?
It helps remove paper, aluminum, gels, fines, black specks, and degraded material while preserving throughput and protecting the die and downstream equipment from contamination-related instability.
How do controls affect recycling extrusion performance?
Controls influence startup repeatability, pressure stability, monitoring, and how quickly operators can respond to process drift caused by variable recycled feed quality.
Do I also need measurement and inspection systems?
Yes. Melt delivery and filtration improve the process, but measurement and inspection systems help verify whether process changes are actually improving product quality.
How does upstream resin handling affect melt delivery?
Inconsistent conveying, blending, feeding, or material preparation upstream can create variability that no downstream melt-delivery system fully cancels out.
Gauge Advisor helps recycling and regrind processors evaluate MAAG equipment for pressure stability, contamination control, and more consistent production.
Need Help Evaluating a Recycling Extrusion Upgrade?
Send your material type, contamination concerns, recycled content, throughput, filler level, and line configuration. Describe the problem you want to solve so Gauge Advisor can help narrow the equipment options.
What to Send for a Faster Recommendation
The fastest way to evaluate a recycling extrusion application is to share the polymer type, contamination concerns, reclaimed or post-consumer content, current throughput, filler load, line configuration, and what issue matters most: contamination handling, pressure instability, uptime, startup scrap, or operator burden.